Pharmaceutical Box Overwrapping Equipment Solutions

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Mobile
Describe Yourself
Message
0/1000

pharmaceutical box overwrapping equipment

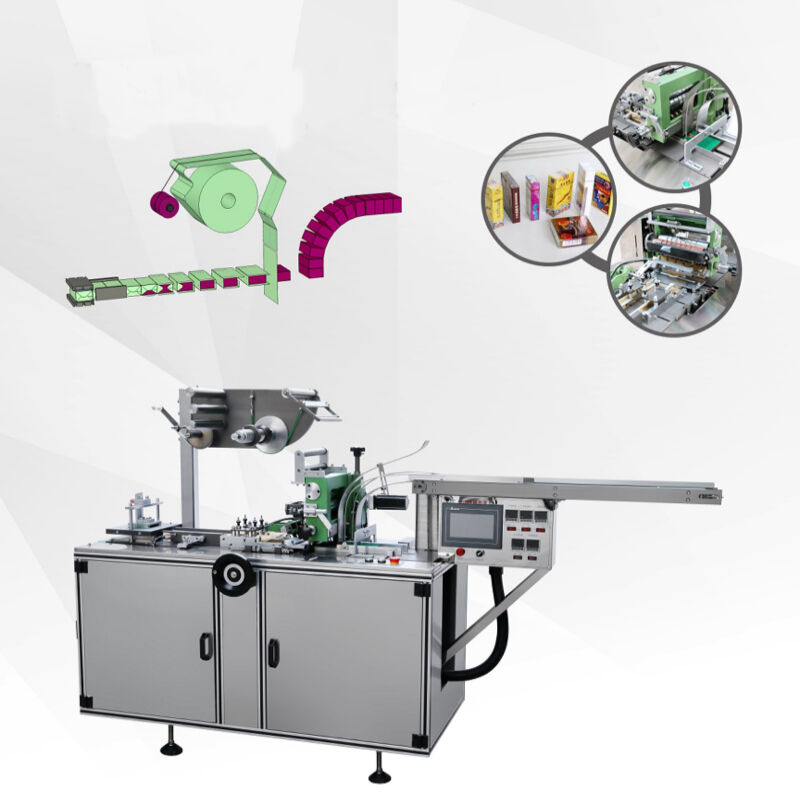
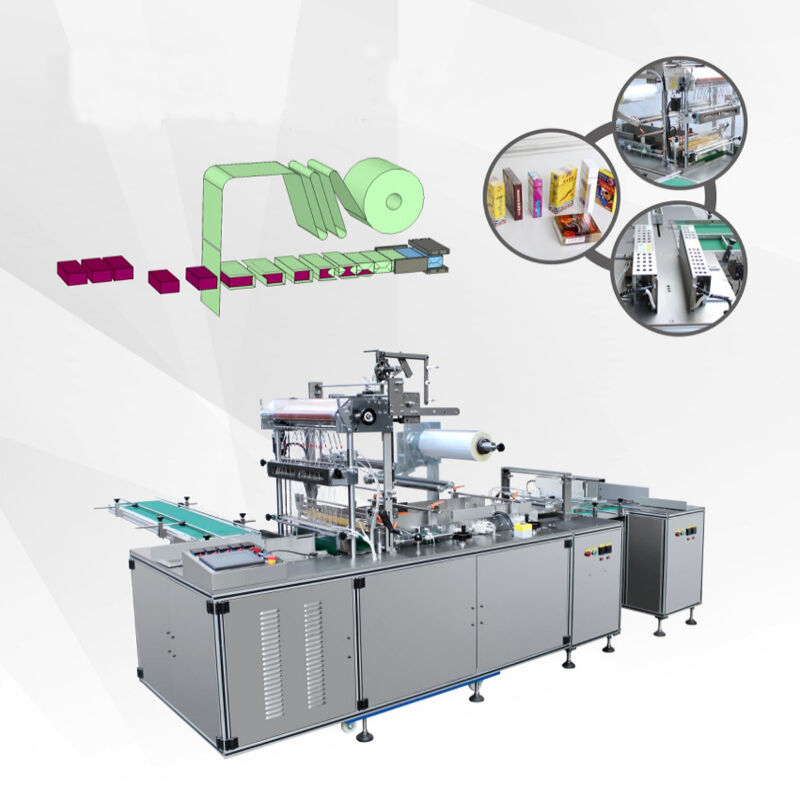
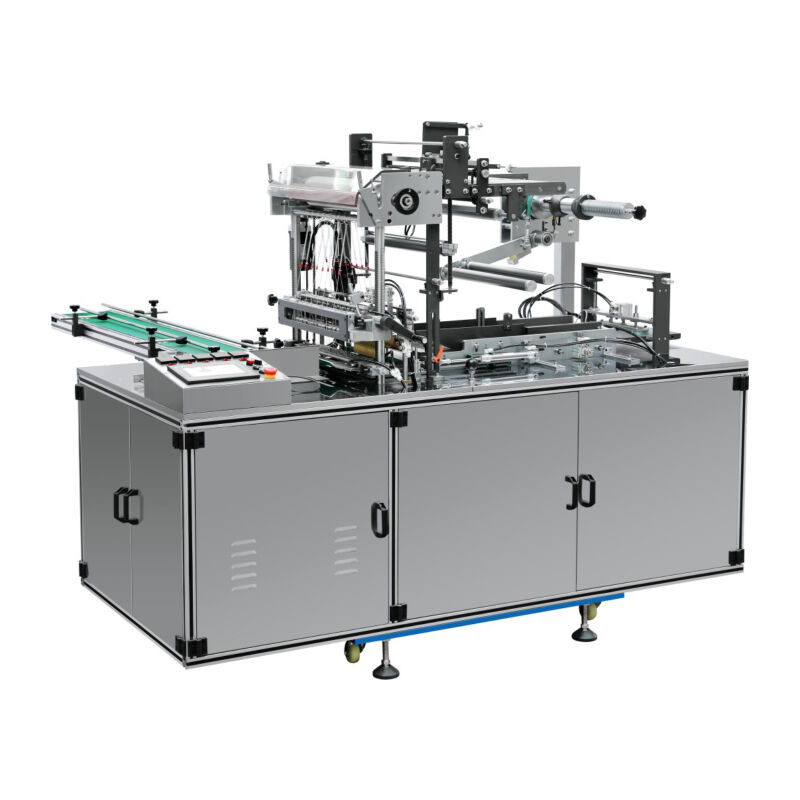
Pharmaceutical box overwrapping equipment is specialized packaging machinery designed to apply transparent film around pharmaceutical product boxes, creating a protective seal that ensures product integrity and regulatory compliance. This equipment automates the process of wrapping individual cartons with a tight, tamper-evident layer that safeguards medications from moisture, dust, contamination, and unauthorized access throughout the supply chain. The pharmaceutical box overwrapping equipment utilizes advanced servo motor controls and precision folding mechanisms to deliver consistent wrapping results at high speeds while maintaining gentle handling of delicate packaging materials. Modern systems feature touchscreen interfaces with recipe management capabilities, allowing operators to quickly switch between different box sizes and film specifications without extensive manual adjustments. The technology incorporates automatic feeding systems that orient and position boxes correctly before wrapping, heat-sealing units that create secure closures, and quality inspection sensors that detect wrapping defects in real-time. These machines are engineered to meet stringent pharmaceutical manufacturing standards including FDA compliance and Good Manufacturing Practice requirements. Applications span across various pharmaceutical segments including prescription medications, over-the-counter drugs, nutraceuticals, medical devices, and healthcare products. The pharmaceutical box overwrapping equipment integrates seamlessly into existing production lines, connecting with upstream cartoning machines and downstream case packers to create fully automated packaging workflows that enhance productivity while reducing labor costs and human error in pharmaceutical manufacturing facilities.
New Product Releases

Investing in pharmaceutical box overwrapping equipment delivers immediate operational improvements that directly impact your bottom line and product quality. The automated wrapping process eliminates manual labor requirements, reducing packaging costs by up to sixty percent while simultaneously increasing throughput capacity to handle growing production demands. Your facility gains enhanced product protection as the tight film barrier shields medications from environmental factors that could compromise efficacy, reducing product returns and waste. The tamper-evident seal created by pharmaceutical box overwrapping equipment builds consumer confidence and satisfies regulatory requirements across global markets, expanding your distribution opportunities. Operational efficiency improves dramatically as these machines maintain consistent wrapping quality regardless of operator skill level, eliminating the variability associated with manual processes. Changeover times decrease substantially through intuitive digital controls that store multiple product specifications, allowing your team to switch between different packaging formats in minutes rather than hours. The equipment adapts to various box dimensions and film materials, providing flexibility as your product portfolio evolves without requiring additional capital investment. Energy-efficient heating systems and optimized film usage minimize operating expenses while supporting sustainability initiatives. Real-time monitoring capabilities provide production data that helps identify bottlenecks and optimize workflow efficiency. The compact footprint of modern pharmaceutical box overwrapping equipment maximizes valuable cleanroom space, and the enclosed design contains dust and debris to maintain pharmaceutical-grade environmental standards. Minimal maintenance requirements and robust construction ensure high uptime rates that keep production schedules on track, while the intuitive operation reduces training time for new personnel, accelerating workforce productivity and maintaining consistent output quality across shifts.

Tips And Tricks

Breakthrough in Tobacco Packaging: Advanced Cigarette Cellophane Wrapping Machine Redefines Efficiency & Precision

21

Apr

Breakthrough in Tobacco Packaging: Advanced Cigarette Cellophane Wrapping Machine Redefines Efficiency & Precision

View More
Innovation in Perfume Packaging: Advanced Cellophane Wrapping Machine Elevates Luxury & Efficiency

21

Apr

Innovation in Perfume Packaging: Advanced Cellophane Wrapping Machine Elevates Luxury & Efficiency

View More
Yiwu Jiedu Machinery Equipment Launches Advanced Cellophane Wrapping Machine, Redefining Perfume Packaging Efficiency & Luxury

22

Apr

Yiwu Jiedu Machinery Equipment Launches Advanced Cellophane Wrapping Machine, Redefining Perfume Packaging Efficiency & Luxury

View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Mobile
Describe Yourself
Message
0/1000

pharmaceutical box overwrapping equipment

Advanced Servo Control Technology

Advanced Servo Control Technology

The pharmaceutical box overwrapping equipment incorporates state-of-the-art servo motor technology that delivers unmatched precision and reliability in every wrapping cycle. Unlike traditional mechanical drive systems, servo controls provide independent adjustment of each machine function, enabling precise synchronization between feeding, folding, sealing, and cutting operations. This technology allows the equipment to automatically adjust wrapping parameters in real-time based on box dimensions and film characteristics, ensuring optimal tension and seal quality without operator intervention. The servo system reduces film waste by calculating exact material requirements for each package, delivering cost savings that accumulate significantly over production runs. Enhanced acceleration and deceleration control protects delicate pharmaceutical packaging from damage during handling, reducing product rejection rates. The system operates quietly compared to conventional machinery, improving workplace conditions in pharmaceutical manufacturing environments. Diagnostic capabilities built into the servo controllers provide predictive maintenance alerts that prevent unexpected downtime, while the digital precision ensures repeatable performance that meets stringent pharmaceutical validation requirements for packaging processes, making this feature essential for facilities pursuing regulatory compliance and operational excellence.
Integrated Quality Verification Systems

Integrated Quality Verification Systems

Modern pharmaceutical box overwrapping equipment features sophisticated quality verification systems that automatically inspect every wrapped package to ensure complete seal integrity and proper film application. Advanced vision sensors detect even microscopic wrapping defects including incomplete seals, film tears, improper folds, or contamination before products proceed to downstream processes. This integrated quality control eliminates the need for manual inspection, reducing labor requirements while providing more reliable defect detection than human visual checks. The system automatically rejects substandard packages, diverting them from the production line to prevent non-conforming products from reaching distribution channels. Statistical process control software analyzes quality data in real-time, identifying trends that might indicate developing issues before they result in significant product loss. Documentation capabilities generate comprehensive packaging records that support regulatory audits and traceability requirements throughout pharmaceutical supply chains. The verification system validates that tamper-evident features function correctly, protecting brand reputation and consumer safety. For pharmaceutical manufacturers operating under strict quality management systems, these integrated verification capabilities provide the documentation and assurance necessary to maintain certification while reducing quality control costs and accelerating batch release times through automated validation processes.
Hygienic Design for Pharmaceutical Environments

Hygienic Design for Pharmaceutical Environments

The pharmaceutical box overwrapping equipment is engineered specifically for pharmaceutical manufacturing environments with construction features that support cleanroom operations and sanitation protocols. Stainless steel contact surfaces resist corrosion and facilitate thorough cleaning between product changeovers, preventing cross-contamination risks in facilities producing multiple pharmaceutical products. The enclosed machine architecture contains film particles and dust generated during operation, maintaining the controlled environment essential for pharmaceutical packaging. Smooth surfaces without crevices or dead spaces eliminate areas where contaminants could accumulate, simplifying validation of cleaning procedures. Tool-free access panels enable rapid inspection and cleaning without introducing foreign objects that could contaminate pharmaceutical products. The equipment meets international pharmaceutical equipment standards with certifications that demonstrate compliance with regulatory requirements across multiple jurisdictions. Sealed electrical components and IP-rated enclosures protect sensitive controls from cleaning agents used in pharmaceutical sanitation procedures. The hygienic design reduces microbial contamination risks while simplifying compliance with Good Manufacturing Practice regulations. For pharmaceutical companies investing in packaging automation, this specialized construction ensures the equipment supports rather than compromises the stringent cleanliness standards essential to pharmaceutical production, protecting product quality and regulatory standing while enabling efficient automated packaging operations.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Mobile
Describe Yourself
Message
0/1000